Company name: Dalian Plastics Research Institute Co., Ltd
Telephone:+86-411-66177850
18841186255
Fax:+86-411-86601784
Address: No.18 Fenghenan Road,Lvshunkou District,Dalian,Liaoning
Company name: Dalian Plastics Research Institute Co., Ltd
Telephone:+86-411-66177850
18841186255
Fax:+86-411-86601784
Address: No.18 Fenghenan Road,Lvshunkou District,Dalian,Liaoning
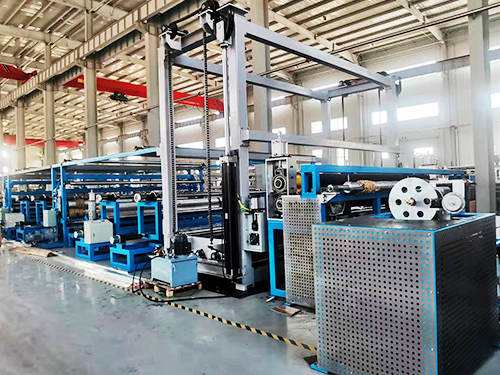
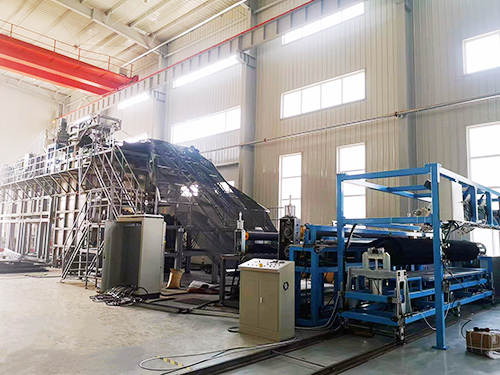
The gluing uniformity of honeycomb panel production line equipment directly affects the bonding effect between core material and face sheet. Excessively thick glue causes glue overflow and panel contamination, while too thin glue leads to glue shortage and weak bonding. Controlling gluing uniformity is a key point in commissioning and daily maintenance of honeycomb panel production lines.
Before formal startup, complete glue pretreatment and glue supply system inspection. The temperature and viscosity of glue change its flow behavior. Excessively high viscosity results in poor fluidity, causing broken glue strips and uneven coating; excessively low viscosity makes the glue run and the glue layer thinner. Set the corresponding temperature range according to the glue type, keep continuous stirring to prevent filler sedimentation and delamination. Clean glue supply pipelines and filters regularly, as accumulated impurities will block glue outlets and cause local glue interruption. For honeycomb panel production line equipment, the glue shall be kept at constant temperature and stand still in advance at the feeding stage, filtered before being pumped into the glue pump to reduce coating fluctuation caused by the glue itself.
Select the coating method according to the process and match the corresponding adjusting mechanism. Common coating types include roll coating, curtain coating and dispensing spraying, with different adjustment modes for different structures. Roll coating controls glue application amount by the gap between glue roller and metering roller; the parallelism of the two rollers and roller roundness are fundamental. Curtain coating stabilizes the glue curtain by overflow knife gap and supply flow rate. Continuous dispensing matches glue output through valve switching frequency and travelling speed. When producing panels of different thicknesses or using different glue systems on honeycomb panel production line equipment, fix the coating structure preferentially and avoid random replacement of coating methods to prevent loss of uniformity control.
Calibrate roller gap and parallelism to set the benchmark of glue thickness. For roll coating, the gaps at both ends of metering roller and coating roller shall be consistent. Large gap difference between two ends results in uneven thickness from side to side. Measure the roller gap section by section with feeler gauges, fine-tune the adjusting handwheels at both ends, and check the roller surface for wear and pits. Damaged roller surfaces produce periodic glue thickness stripes. The roller speed shall be synchronized with panel conveying speed. Excessive difference between roller linear speed and panel travelling speed easily causes stretching or accumulation of glue layer. During commissioning of honeycomb panel production line equipment, perform idle roller test first, observe the glue carrying condition of rollers, and feed panels for trial coating only after continuous and unbroken glue film is formed.
Stabilize glue supply pressure and flow rate to eliminate output fluctuation. Unstable glue pump pressure leads to varying glue output per unit time. Adopt a stabilized pressure supply scheme with pressure sensor feedback adjustment to maintain stable pipeline pressure. For dual-channel or multi-channel simultaneous gluing, keep consistent pressure of each channel to avoid inconsistent glue volume on left and right sides of panels. Unify the length and bending degree of hoses as much as possible to reduce difference in pipeline resistance. Avoid frequent start-stop of glue pumps during operation of honeycomb panel production line equipment; pressure impact at start and stop easily causes abnormal gluing at the start and end sections.
Control panel conveying and positioning to reduce feeding deviation. Panel wandering or unstable conveying speed will cause local uneven glue layer even if the coating unit works normally. Keep consistent tightness of conveying rollers, stable belt tension and properly adjusted side guiding limit devices to ensure panels pass through the coating station centrally at a constant speed. Panel flatness also has an impact: warped or sunken panel areas cannot fit closely with rollers, resulting in thin glue layers. Inspect panels before feeding and sort out deformed panels in advance to avoid continuous gluing defects in mass production.
Control environmental parameters to reduce difference in glue curing rate. Workshop temperature and humidity affect the levelling time of glue. High temperature accelerates curing; glue sets before adequate levelling and tends to form strip marks. High humidity delays curing of some glue types and makes glue flow and thicken. Keep the coating station away from strong direct air blow, as air disturbance will damage the glue film. During long-time continuous production of honeycomb panel production line equipment, sample and inspect panels regularly and compare with the first sample. Once abnormal levelling occurs, fine-tune the environment or coating speed to reserve proper levelling time for glue.
Adopt on-line monitoring and regular maintenance to sustain gluing quality. Vision or thickness detection devices can be equipped to identify glue shortage, excessive thickness and stripe defects in real time. Daily inspection focuses on roller surface cleaning; dried glue scale on rollers damages the glue film. Regularly clean cured glue residue on dispensing valves and knife gaps. Re-test panels and recheck uniformity after glue type or panel specification replacement. If periodic unevenness appears, prioritize checking roller damage and bearing runout; for irregular thickness fluctuation, focus on glue supply pressure and glue viscosity.
In summary, to control gluing uniformity for honeycomb panel production line equipment, manage glue viscosity, calibrate coating roller gap and parallelism, stabilize glue supply pressure and conveying speed, provide proper levelling conditions, and implement on-line inspection and regular maintenance. Stable glue thickness is guaranteed to secure the bonding quality of honeycomb panels.



Address: No.18 Fenghenan Road,Lvshunkou District,Dalian,Liaoning Telephone:18841186255 mailbox:dsy@plasticdl.com

 Taobao Wangwang