Company name: Dalian Plastics Research Institute Co., Ltd
Telephone:+86-411-66177850
18841186255
Fax:+86-411-86601784
Address: No.18 Fenghenan Road,Lvshunkou District,Dalian,Liaoning
Company name: Dalian Plastics Research Institute Co., Ltd
Telephone:+86-411-66177850
18841186255
Fax:+86-411-86601784
Address: No.18 Fenghenan Road,Lvshunkou District,Dalian,Liaoning
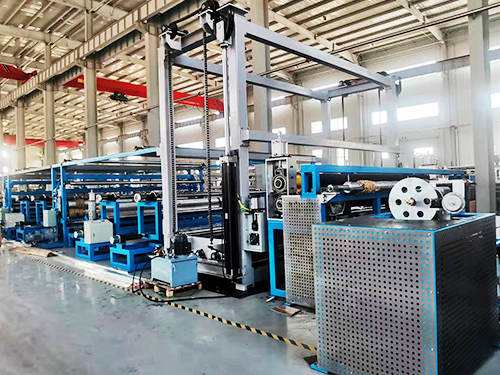
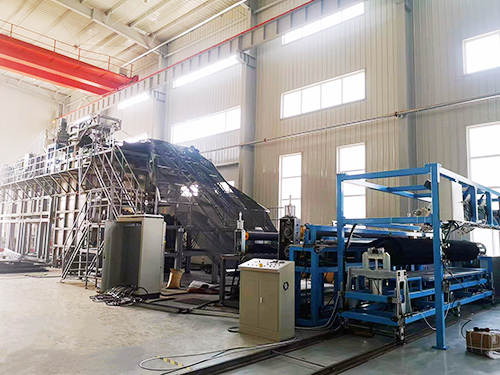
The biaxial stretching mesh production line is continuous extrusion molding equipment. During production, factors including raw materials, temperature, traction speed and die condition affect mesh forming. Proper troubleshooting cuts downtime and stabilizes production. Inspections shall follow the sequence: external observation first, parameter verification second, and component disassembly last, to prevent secondary issues caused by blind operations.
Before startup, operators shall conduct basic checks to reduce potential faults. Focus on raw material feeding: ensure no agglomerates or impurities in hoppers and smooth feeding channels. Damp or contaminated raw materials lead to unstable screw feeding and intermittent discharge. Verify temperature readings of heating zones, check stability of temperature controllers and loose connections of heating rings and thermocouples. Temperature fluctuations change melt fluidity and cause uneven mesh filament thickness.
During operation, focus on extrusion and die head. Uneven die discharge, broken or missing mesh ribs are usually caused by carbon deposits on die lips, which alter melt gaps. Clean the die only after the equipment cools to a safe temperature. Check matching of screw speed and traction speed. Mismatched parameters lead to abnormal stretching ratios and off-spec mesh openings. If extrusion pressure keeps rising, inspect filter assemblies; replace clogged filters periodically.
The stretching unit is the core of the line, with faults mainly on traction and stretching roller sets. Mesh deviation may result from residual deposits, roller wear or unbalanced pressure on roller ends. Residues on rollers change friction and cause side drift. Mesh rupture relates not only to raw materials but also transverse and longitudinal stretching ratios. Excessively fast stretching exceeds material tolerance. Inspect chains and drive belts for looseness or abnormal noise; varying clearances of transmission parts cause speed fluctuation and poor forming stability.
Faults in cooling and sizing affect product appearance and dimensional stability. Temperature fluctuations of cooling tanks or rolls create inconsistent cooling rates and mesh warpage. Check cooling water circulation and pump operation, and remove scale deposits. Insufficient cooling leads to incomplete sizing and deformation during winding.
Troubleshooting for winding and detection targets uneven or inconsistent rolls. Check the tension control system for fluctuating tension, inspect tension sensors and guide rollers. Stuck guide rollers change conveying resistance and cause bulges or wrinkles. Abnormal noise or vibration requires immediate shutdown to inspect lubrication of bearings and reducers and replenish or replace lubricant.
Keep records of fault symptoms, root causes and solutions after troubleshooting. Historical records help maintenance teams identify equipment wear patterns and schedule maintenance. Regular cleaning and timely replacement of wearing parts reduce recurring faults. Operators shall master equipment structure, follow shutdown maintenance rules and ensure safety during the whole troubleshooting process.



Address: No.18 Fenghenan Road,Lvshunkou District,Dalian,Liaoning Telephone:18841186255 mailbox:dsy@plasticdl.com

 Taobao Wangwang